Why Time-Based Depreciation Fails on High-Flow Printers and Composites
Tracking nozzle wear by printing hours fails completely on modern high-speed CoreXY printers extruding 22 mm³/s and running abrasive fiber composites.
Traditional 3D printing cost accounting allocated machine depreciation strictly by printing hours ($0.25/h). On a modern CoreXY printer running at 250–350 mm/s with a volumetric flow rate exceeding 22 mm³/s, the machine pushes three to four times more plastic through the hotend per hour than an older Cartesian printer.
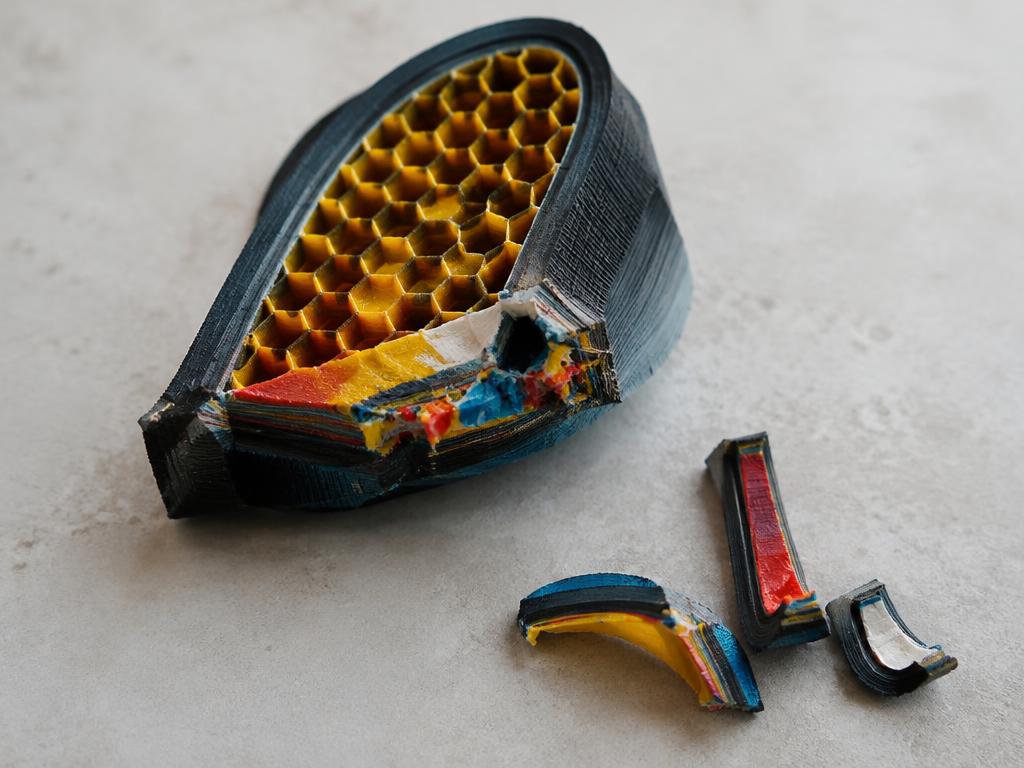
Furthermore, carbon fiber (CF), glass fiber (GF), phosphorescent glow additives (strontium aluminate), and wood composites behave like liquid sandpaper. A standard brass nozzle can be ruined in less than 400 grams of glow or CF filament, widening the orifice from 0.40 mm to 0.65 mm and causing severe under-extrusion and dimensional failure.
- Volumetric Throughput: High-flow hotends extrude 20–30 grams per hour versus 6–10 grams on older equipment.
- Abrasive Particle Action: Chopped carbon fibers and strontium aluminate cristals erode nozzle orifices and extruder drive gears.
- PEI Coating Wear: Frequent thermal cycling and aggressive scraper adhesion strip the textured PEI film over time.
The Volumetric Tooling Surcharge Formula: Amortizing Wear per Kilogram
Tooling and build surface wear must be calculated as a direct consumable surcharge added per kilogram of filament extruded, categorized across 4 abrasiveness families.
To protect workshop profitability, nozzle replacement costs and PEI build plate degradation should be amortized directly into the spool unit cost. When printing technical composites, hardened steel or ruby nozzles and hardened extruder gears are non-negotiable investments.
By establishing a per-kilogram tooling surcharge, every gram extruded automatically finances replacement hotends, hardened extruder drive wheels, and replacement build sheets.
FXTechnical Breakdown · How InfillQuote calculates this behind the scenes (View formula)▼
\text{Surcharge}_{\text{tooling}}/\text{kg} = \frac{\text{Hotend Nozzle Cost}}{\text{Useful Lifespan (kg)}} + \frac{\text{PEI Sheet Cost}}{\text{Useful Lifespan (Spools)}}For a $35 hardened steel hotend lasting 12 kg of PA-CF and a $25 PEI sheet lasting 15 spools: ($35 / 12) + ($25 / 15) = $2.92 + $1.67 = $4.59/kg surcharge ($0.0046/gram).
| Material Family | Nozzle Lifespan | PEI Sheet Lifespan | Surcharge (BRL) | Surcharge (USD) | Surcharge (EUR) | Tooling Requirements |
|---|---|---|---|---|---|---|
| Standard PLA / PETG / TPU | 40–80+ kg | 60–100 spools | +R$ 2,50/kg | +$0.50/kg | +€0.45/kg | Standard brass nozzle and textured PEI sheet. |
| Wood PLA / Marble / White Titanium TiO2 | 15–25 kg | 35–50 spools | +R$ 6,00/kg | +$1.20/kg | +€1.10/kg | Hardened brass or plated copper; mild abrasive pigments. |
| Composites (PLA-CF, PETG-CF, ABS-GF, PA-CF) | 8–15 kg | 20–30 spools | +R$ 15,00/kg | +$3.00/kg | +€2.75/kg | Hardened steel nozzle and hardened extruder gears mandatory. |
| Phosphorescent (Glow) & Metal Filled | 4–10 kg | 12–20 spools | +R$ 22,00/kg | +$4.50/kg | +€4.00/kg | Severe wear; rapid erosion of PTFE tubes, extruder gears, and AMS funnels. |
Table: The 4 Material Abrasiveness Families & Kilogram Tooling Surcharges
Note: Surcharges must be added to raw filament spool costs inside your quoting engine.
Protecting AMS Funnels, PTFE Tubes & Incorporating Surcharges in InfillQuote
Abrasive filaments also grind internal PTFE bowden tubes and AMS entry funnels, requiring replacement every 15–20 spools or the installation of ceramic wear protectors.
Workshops utilizing automatic multi-material systems (like Bambu AMS) frequently overlook wear along the filament path. Stiff carbon fiber strands and gritty glow filaments slice through curved PTFE tubing and carve grooves into plastic AMS feeder funnels, triggering feed jams and motor stalls.
In InfillQuote, simply add the tooling surcharge directly onto the filament entry price in your material catalog (e.g., entering a $28/kg PETG-CF spool at $31/kg). This guarantees that every single gram billed through customer quotes automatically provisions future tooling and maintenance.
- PTFE Tube Inspection: Replace reverse bowden tubes when internal grooving causes mechanical friction.
- Ceramic Funnel Protectors: Install snap-on stainless steel or ceramic inserts at AMS filament entry funnels.
- Automated Surcharge in InfillQuote: Embed the tooling wear surcharge directly into spool catalog pricing.
Frequently Asked Questions
How many grams of Glow-in-the-Dark filament will destroy a standard brass nozzle?
As few as 250 to 500 grams. Strontium aluminate crystals have a Mohs hardness of 8 (harder than hardened carbon steel). Passing half a spool of glow filament through a brass nozzle will erode the orifice bore, ruining print tolerance and surface quality.
Why do textured PEI sheets degrade over thermal and chemical cycles?
Repeated heating and cooling cycles above 80°C (for PETG, ABS, and Nylon) gradually weaken the adhesion between the spring steel substrate and the sprayed PEI coating. Aggressive scraping and petro-chemical residues further strip the texture, leading to bed adhesion failure.
How do I incorporate this tooling surcharge into InfillQuote?
Navigate to your Material Presets in InfillQuote. When creating or editing an abrasive spool (e.g., PLA-CF, PETG-CF, Glow), increase the purchase price by the family surcharge (+$3.00/kg to +$4.50/kg). The pricing engine will automatically factor this into all future quotes.