Where 40% of Margin Disappears: The Real Anatomy of Post-Processing
Manual post-processing regularly accounts for 30% to 40% of the true cost of a finished part, broken down into support removal, progressive sanding, chemical treatment, and inspection.
Many workshops calculate print costs with razor-sharp accuracy in the slicer, only to watch their net profit evaporate at the workbench. A part that took $3.00 of filament and 4 machine hours can easily demand 35 minutes of hands-on labor to remove tree supports, trim brims, wet-sand layer steps, and apply primer.
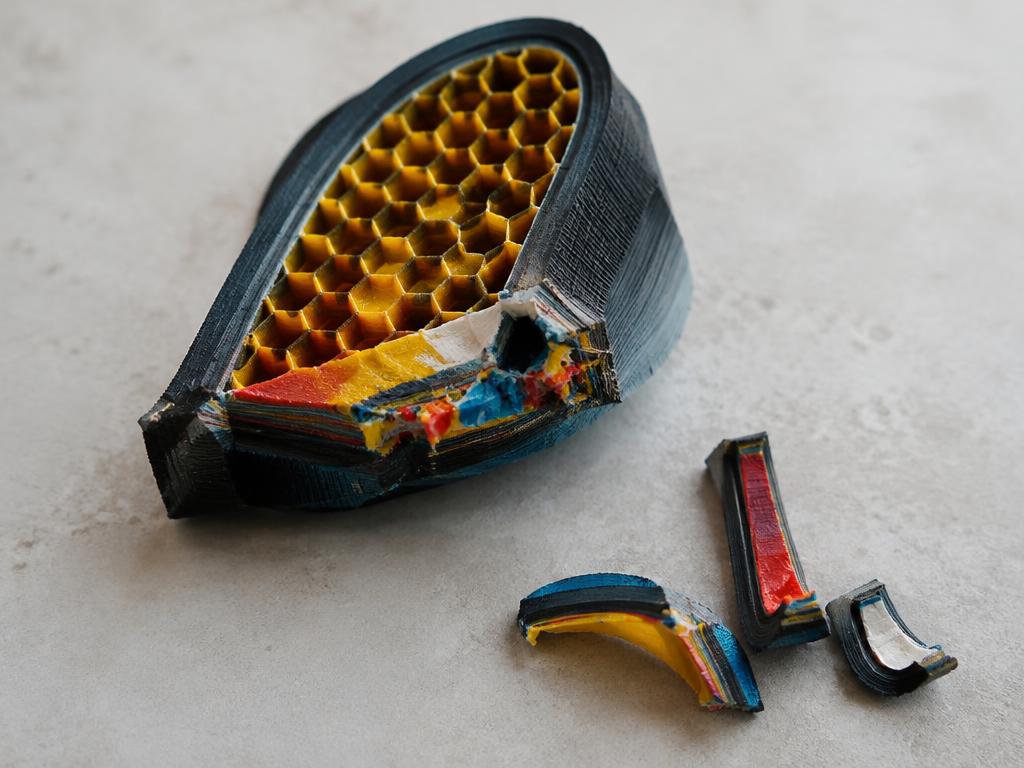
Empirical workshop studies show that manual post-processing time divides predictably: support stripping and brim trimming (35%–45%), progressive sanding from 120 to 1200 grit (25%–35%), chemical smoothing, heat-set insert installation, or spray painting (15%–25%), and dimensional inspection (10%–15%). Ignoring these workbench minutes turns high-value prints into uncompensated hobby projects.
- Support & Brim Removal (35%–45% of bench time): Flush cutters, deburring blades, needle-nose pliers.
- Progressive Sanding (25%–35% of bench time): Dry shaping (120–240 grit) transitioning to wet sanding (400–1200 grit).
- Chemical & Thermal Operations (15%–25% of bench time): Acetone/IPA vapor, heat-set brass threaded inserts, filler primer, topcoats.
- Quality & Dimensional Inspection (10%–15% of bench time): Digital caliper verification and thread checking.
The 3 Commercial Finishing Tiers & Chemical Consumables Formula
Every quotation must categorise surface finish into 3 distinct commercial tiers: As-Built, Standard Prep, or Premium Studio, pricing both active minutes and consumable overhead.
Offering a single ambiguous finishing standard invites endless client friction. By defining three concrete tiers, clients choose their aesthetic tolerance upfront, paying directly for the labor and chemical consumables required.
Consumable costs (sandpaper discs, masking tape, filler primer spray cans, solvent wipes, nitrile gloves) cannot be absorbed. They must be amortized alongside active labor minutes.
FXTechnical Breakdown · How InfillQuote calculates this behind the scenes (View formula)▼
\text{Cost}_{\text{finish}} = \left( \frac{\text{Active Minutes}}{60} \times \text{Labor Rate} \right) + \text{Chemical Consumables}For a 30-minute Standard Prep at $37.14/h with $2.50 in sandpaper and primer consumables: (30/60 × $37.14) + $2.50 = $18.57 + $2.50 = $21.07 finishing surcharge.
| Finishing Tier | Active Bench Time | Consumables Overhead | Price Multiplier | Surface Description & Scope |
|---|---|---|---|---|
| Tier 1: As-Built (Bruto de Máquina) | 5–10 min | $0.15 (R$ 0,50 / €0.15) | 1.0x (Base Price) | Brim and support contact points trimmed; layer lines visible; dimensional fit verified. |
| Tier 2: Standard Prep (Técnico Alisado) | 25–45 min | $2.00–$3.50 (R$ 8–15 / €1.80–3.20) | 1.45x–1.80x (+45% to +80%) | Wet-sanded up to 400 grit; 1–2 coats of filler primer; seam lines minimized and paint-ready. |
| Tier 3: Premium Studio (Exposição & Pintura) | 120–360+ min | $5.00–$14.00 (R$ 25–65 / €4.50–12.50) | 2.0x–5.0x (+100% to +400%) | Wet-sanded up to 1200 grit; multi-layer airbrush painting, clear coat lacquer, automotive finish. |
Table: The 3 Commercial Finishing Tiers & Associated Surcharges
Note: Tier multipliers apply over baseline manufacturing cost before commercial margin.
Slicer Orientation Tactics: How to Cut Bench Time by 30%
Careful slicer orientation eliminates up to 30% of post-processing labor by pointing cosmetic faces upwards and setting top Z support distances between 0.20 mm and 0.24 mm.
The fastest way to lower post-processing costs is preventing support scarring inside the slicer. Orienting critical cosmetic surfaces at angles greater than 45° eliminates the need for support contact along primary sightlines.
Using organic tree supports drastically reduces the contact area compared to traditional rectilinear grids. Setting a top Z-contact distance of 0.20 mm for 0.4 mm nozzles ensures supports snap cleanly off without leaving scarred stubs that require aggressive sanding.
- Face Orientation: Point aesthetic and visible cosmetic surfaces upwards away from build plate supports.
- Top Z Distance: Maintain 0.20–0.24 mm clearance between support roof and printed interface for clean detachment.
- Organic Tree Supports: Use branch angles <= 45° to reach overhangs without touching outer model walls.
- Modular Splitting: Cut complex geometries into aligned pin-jointed halves to print completely support-free.
Frequently Asked Questions
How should I charge for sandpaper, filler primer, and adhesives on individual parts?
Standardize consumable overhead per tier. For Tier 1 (As-Built), add a nominal $0.15/part for utility blades and gloves. For Tier 2 (Standard Prep), budget $2.50/part for abrasive sheets and primer can fractions. For Tier 3, track primer, paint, and clear lacquer usage at $6.00–$12.00 per model.
When is it economically justified to use dedicated support interface filaments in multi-material systems?
When printing high-complexity engineering prototypes with tight internal cavities where manual support removal would take 45+ minutes or risk breaking delicate features. Using PLA as an interface layer for PETG (or dedicated breakaway materials) provides zero-gap support with zero sanding required.
How do resin SLA/MSLA solvent wash and post-curing costs compare to FDM post-processing?
Resin finishing is chemically intensive: each model carries an average 8% IPA solvent loss through evaporation and contamination ($0.40–$0.80/wash cycle), plus 10–20 minutes of ultrasonic washing, support snipping, and UV curing chamber energy and lamp wear.